Jet aerators support oxygen transfer and mixing in aerobic wastewater treatment, but operating them at maximum output does not necessarily improve treatment performance. Efficient operation depends on four factors: matching oxygen supply to biological demand, maintaining effective bubble shearing, combining aeration with mixing, and selecting the equipment according to wastewater characteristics and reactor conditions.
In practice, these factors affect oxygen transfer, energy consumption, hydraulic circulation, and long-term operating stability. Therefore, improving jet aerator efficiency requires more than increasing aeration capacity. Engineers should evaluate the aerator, recirculation pump, nozzle, air supply, reactor geometry, and wastewater characteristics as one integrated system.

Table of Contents
Working Principle and Aeration Efficiency Optimization
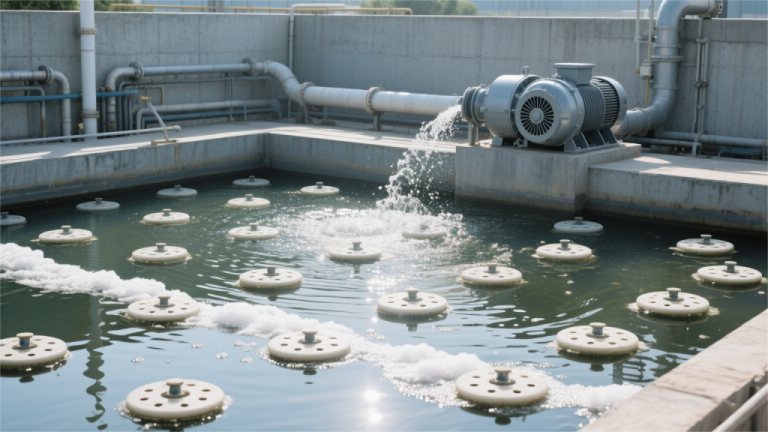
A jet aerator uses a high-velocity liquid jet to create turbulence and mix air with recirculated wastewater. The liquid jet passes through the nozzle and creates strong gas-liquid interaction in the mixing zone. This process disperses air into the wastewater while the resulting jet plume promotes circulation throughout the reactor.
The aerator therefore performs two important functions at the same time: oxygen transfer and liquid mixing. However, its actual performance depends on the equipment configuration, liquid flow, air flow, reactor geometry, wastewater characteristics, and operating conditions.
Strategy 1: Match Aeration Output to Actual Oxygen Demand
Operators sometimes run aeration equipment continuously at full capacity because they assume that more oxygen will always improve biological treatment. However, oxygen demand changes with wastewater loading, biological activity, temperature, and process conditions. Excessive aeration can increase energy consumption without providing a proportional improvement in treatment performance.
A dissolved oxygen (DO) control strategy can provide more precise aeration management. Engineers can install DO sensors at representative locations in the aerobic reactor and connect the measurements to a variable-frequency drive or another suitable control system when the equipment configuration supports flow adjustment.
The target DO should reflect the actual biological process rather than a universal fixed value. Conventional activated sludge systems commonly operate around the 1–3 mg/L range, while processes with specific nitrification requirements may require different conditions. Therefore, operators should establish the DO target according to the treatment process, loading conditions, and biological requirements.
In addition, operators should monitor DO trends rather than relying on a single measurement. Changes in influent loading, temperature, sludge concentration, and biological activity can alter oxygen demand. Adjusting aerator operation according to these changes can help avoid unnecessary aeration.
Strategy 2: Reduce Hydraulic Losses in the Recirculation System
The jet aerator relies on recirculated liquid to generate the high-velocity jet. Consequently, unnecessary pressure loss in the recirculation system can reduce jet velocity and increase the power required from the pump.
For this reason, engineers should consider pipe diameter, pipe length, elevation changes, elbows, valves, nozzle pressure requirements, and pump operating conditions during system design. The recirculation pipeline should provide the required liquid flow without creating excessive hydraulic resistance.
Proper hydraulic design also helps maintain stable jet performance. If the actual flow delivered to the nozzle falls below the design requirement, the aerator may produce weaker mixing and less effective air dispersion. Therefore, pump selection and pipeline design should be completed together with jet aerator sizing.
Technical Sizing: Bubble Shearing and Aeration-Mixing Integration
Strategy 3: Optimize Bubble Shearing for Oxygen Transfer
Bubble size directly affects the gas-liquid contact area and oxygen transfer behavior. A jet aerator creates strong turbulence around the liquid jet, helping disperse air into the wastewater. This gas-liquid interaction increases the contact between air and water while the jet plume continues to circulate the reactor contents.
However, oxygen transfer performance should not be represented by one universal efficiency percentage. Actual performance varies with nozzle configuration, liquid flow, air flow, water depth, temperature, wastewater characteristics, and other operating conditions.
Therefore, engineers should evaluate the complete operating condition when selecting a jet aerator. The required liquid recirculation flow and air flow should match the oxygen demand and mixing requirements of the reactor. Nozzle configuration and jet velocity should also provide sufficient gas dispersion without creating unnecessary hydraulic losses.
These factors become particularly important in industrial wastewater treatment. High concentrations of suspended solids, increased viscosity, oil, fibers, scaling, or abrasive particles can affect nozzle performance and hydraulic conditions. As a result, the equipment should be selected according to the actual wastewater rather than according to nominal aeration capacity alone.
Why Bubble Shearing Matters
Large bubbles generally provide less gas-liquid interfacial area per unit volume and can move rapidly toward the water surface. Effective bubble dispersion can increase the contact area available for oxygen transfer and improve gas-liquid interaction.
For this reason, engineers should evaluate aeration performance together with mixing performance. The aerator, recirculation pump, nozzle, air supply, reactor depth, and wastewater properties all influence the final result. Optimizing only one component may not improve overall system performance if the other components remain mismatched.
Strategy 4: Combine Aeration and Mixing in One System
Traditional wastewater treatment systems may use separate aeration and mechanical mixing equipment. A jet aerator can combine these functions by using the high-velocity liquid jet to generate circulation while simultaneously introducing air into the wastewater.
During operation, the jet supplies oxygen for aerobic biological reactions and promotes liquid and solids circulation. This circulation can help reduce localized settling and improve contact between microorganisms, pollutants, and dissolved oxygen.
Jet aeration systems can be used in activated sludge, SBR, oxidation ditch, extended-aeration, and biological nutrient removal applications. Depending on the system design, the liquid jet can also provide mixing when aeration is temporarily not required.
The engineering advantage is therefore not simply increased aeration. Instead, the system coordinates oxygen transfer and reactor circulation through the same hydraulic process. This can simplify equipment integration and provide more consistent mixing conditions when the system is properly sized.
Maintenance and Application Guide
Maintenance: Protect Nozzle and Mixing Performance
Jet aerator performance can gradually decline when the nozzle or mixing components become worn, scaled, or obstructed. This issue is particularly important when the system treats wastewater containing suspended solids, fibers, grease, or other materials that can affect the flow passage.
Operators should regularly inspect the nozzle, mixing components, recirculation piping, valves, and pump operating conditions. Changes in liquid flow, pump pressure, air flow, and aeration performance can also provide useful indicators of equipment deterioration.
The original article recommends inspecting and cleaning the nozzle and mixing chamber every 3–6 months. However, this interval should be treated as a site-specific recommendation rather than a universal maintenance requirement. Actual inspection frequency should depend on wastewater characteristics, operating hours, fouling tendency, and equipment condition.
Early maintenance can help prevent a gradual decline in jet velocity, air dispersion, and mixing performance. For systems treating abrasive or corrosive wastewater, engineers should also evaluate component materials and wear conditions during routine inspections.
Application in Municipal Wastewater Treatment
Jet aerators can be applied in municipal biological treatment systems where oxygen transfer and mixing are both required. Common applications include activated sludge, SBR, oxidation ditch, extended-aeration, and biological nutrient removal processes.
In these systems, the aerator must provide sufficient oxygen for biological reactions while maintaining adequate circulation throughout the reactor. Engineers should therefore consider reactor volume, wastewater loading, water depth, target DO, peak oxygen demand, and hydraulic circulation when determining the required aeration capacity.
Rather than continuously operating the equipment at maximum output, operators can adjust aeration according to actual process conditions where the control system allows it. This approach helps maintain the required biological environment while avoiding unnecessary aeration.
Application in Industrial Wastewater Treatment
Industrial wastewater treatment often presents more variable operating conditions than municipal treatment. Jet aerators can be considered for biological treatment of wastewater from chemical production, food and beverage processing, pulp and paper manufacturing, pharmaceutical production, and other high-strength industrial processes.
The treatment challenges vary between industries. Chemical wastewater may contain corrosive compounds, while food processing wastewater can contain grease and experience significant fluctuations in organic loading. Pulp and paper wastewater may contain fibers and suspended solids, whereas pharmaceutical wastewater can have variable organic concentrations or compounds that affect biological activity.
These differences make application-specific sizing particularly important. Engineers should evaluate suspended solids, viscosity, oil content, temperature, corrosiveness, scaling tendency, and fouling potential before finalizing the aerator configuration.
A large or open flow passage may help reduce clogging risks in solids-laden wastewater. However, nozzle diameter and hydraulic configuration should always match the required flow, jet velocity, wastewater characteristics, and reactor conditions rather than relying on a universal diameter threshold.
Technical Sizing for Jet Aerators
Proper jet aerator selection should start with the wastewater characteristics and biological treatment requirements. Engineers need to evaluate wastewater flow, BOD/COD loading, ammonia concentration, suspended solids, reactor volume, water depth, temperature, and target DO. These factors help determine the required oxygen transfer capacity and hydraulic circulation performance.
The recirculation flow, air flow, nozzle configuration, and pump operating point should also match the reactor conditions. For wastewater containing high concentrations of suspended solids, oil, fibers, corrosive compounds, or abrasive particles, engineers should additionally consider potential clogging, scaling, corrosion, and wear.
Therefore, the final jet aerator configuration should be based on the complete process conditions rather than selecting equipment according to a single parameter. A properly sized system should provide the required oxygen transfer and mixing performance while maintaining stable hydraulic operation.
Conclusion
Jet aerator efficiency depends on the interaction between oxygen demand, hydraulic performance, bubble dispersion, mixing, and maintenance. The four core strategies are to match aeration output to actual oxygen demand, minimize hydraulic losses, optimize gas-liquid shearing, and integrate aeration with mixing where the process requires it.
For municipal and industrial wastewater projects, engineers should evaluate the complete operating system rather than relying on a single efficiency percentage. Wastewater characteristics, reactor geometry, pump performance, nozzle configuration, air supply, and target DO should all be considered during system design.
Ultimately, efficient jet aeration is not about simply increasing aeration intensity. It is about matching the equipment and operating conditions to the actual treatment requirements. Proper sizing, hydraulic design, process control, and regular maintenance can help the system maintain stable oxygen transfer and mixing performance throughout operation.
Talk to Our Wastewater Treatment Engineer
Need help selecting a jet aerator for your wastewater application? Share your flow rate, reactor volume, wastewater characteristics, SS/BOD/COD loading, and target DO. Our engineering team can review your operating conditions and provide a suitable jet aerator configuration and sizing recommendation.
Get a Free Engineering Consultation & Sizing Calculation. We aim to respond within 24 hours, and your project information will be kept confidential.
Last Updated: September 1, 2026
Sources: U.S. EPA aeration guidance; U.S. EPA aeration equipment evaluation; peer-reviewed research on jet aerator oxygen transfer.